Aenlunte Intelligent Fruit Vinegar Equipment
Unlock High-Efficiency Fruit Vinegar Brewing
Fruit vinegar is increasingly favored by consumers for its rich fruit aroma and refreshing taste. However, traditional fruit vinegar brewing has long been plagued by industry pain points including lengthy fermentation cycles, low alcohol-to-acid conversion rate, heavy loss of fruit aroma and unstable quality. How to balance production efficiency and original fruit flavor has become an urgent challenge for fruit vinegar processors. Relying on its core patented technology An Automatic Vinegar brewing equipment (Patent No.: ZL 2016 2 0632 438.6), Enlent offers a mature solution for the industrial production of fruit vinegar and fruit vinegar beverages.
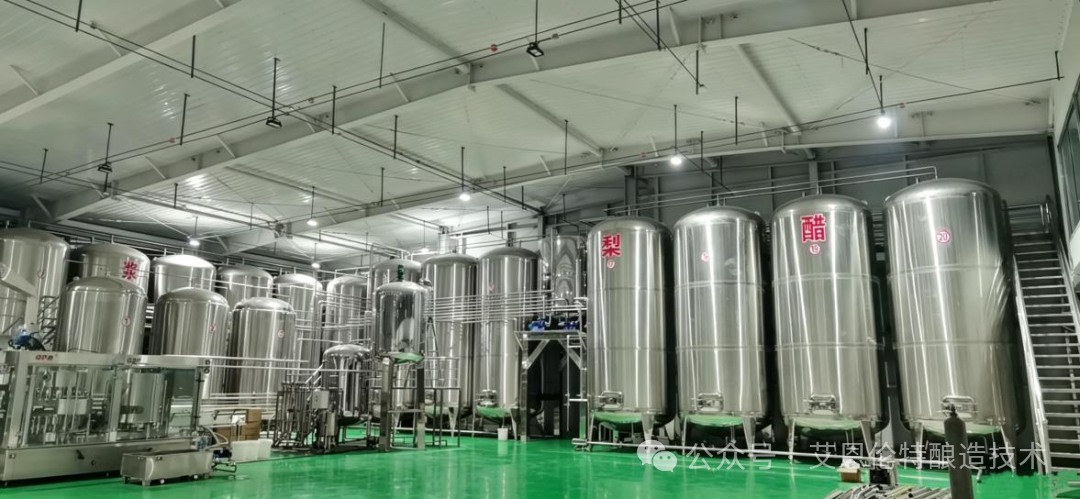
This patented equipment is a robust R&D achievement of Enlent’s in-depth engagement in the brewing sector and a core powerhouse for industrial fruit vinegar production. The main unit is fabricated from SUS304 food-grade Stainless steel with mirror polishing on exterior surfaces. The tank is equipped with a polyurethane foam thermal insulation layer. The whole machine integrates multiple functional modules: cooling system, rotary spraying system, air filtration, acid gas recovery, liquid level indication, immobilized bacterial bed, aseptic sampling and material circulation. Controlled by a single-chip microcomputer or SIEMENS PLC automatic control system, it realizes full-process automatic management of brewing.
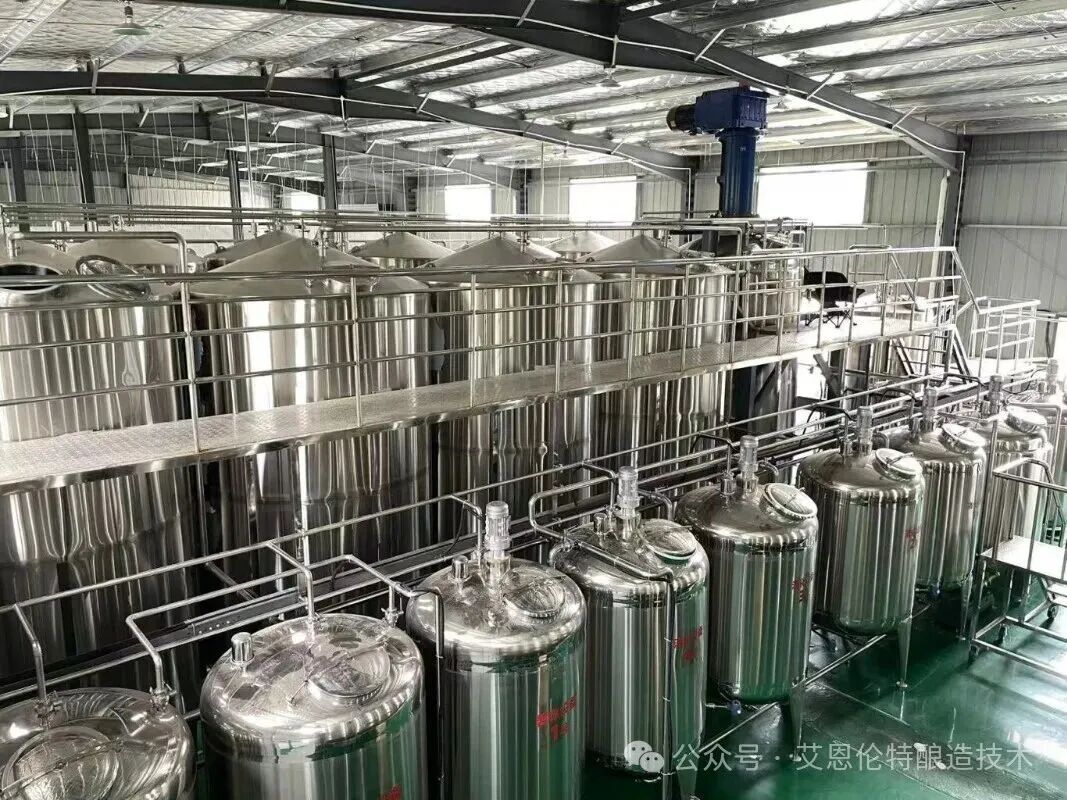
Supported by this patented liquid fermentation process, the fruit vinegar production workflow achieves disruptive optimization. Fresh fruits are processed into fruit juice or concentrated fruit juice. After adjusting the proper total sugar content and temperature control, alcoholic fermentation proceeds. Then acetic fermentation is carried out via the equipment’s exclusive segmented vinegar-Harvesting fermentation method. No exogenous nutrients are required. Acetic fermentation can be completed within 8–24 hours, and finished fruit vinegar with authentic taste can be obtained in around 20 hours.
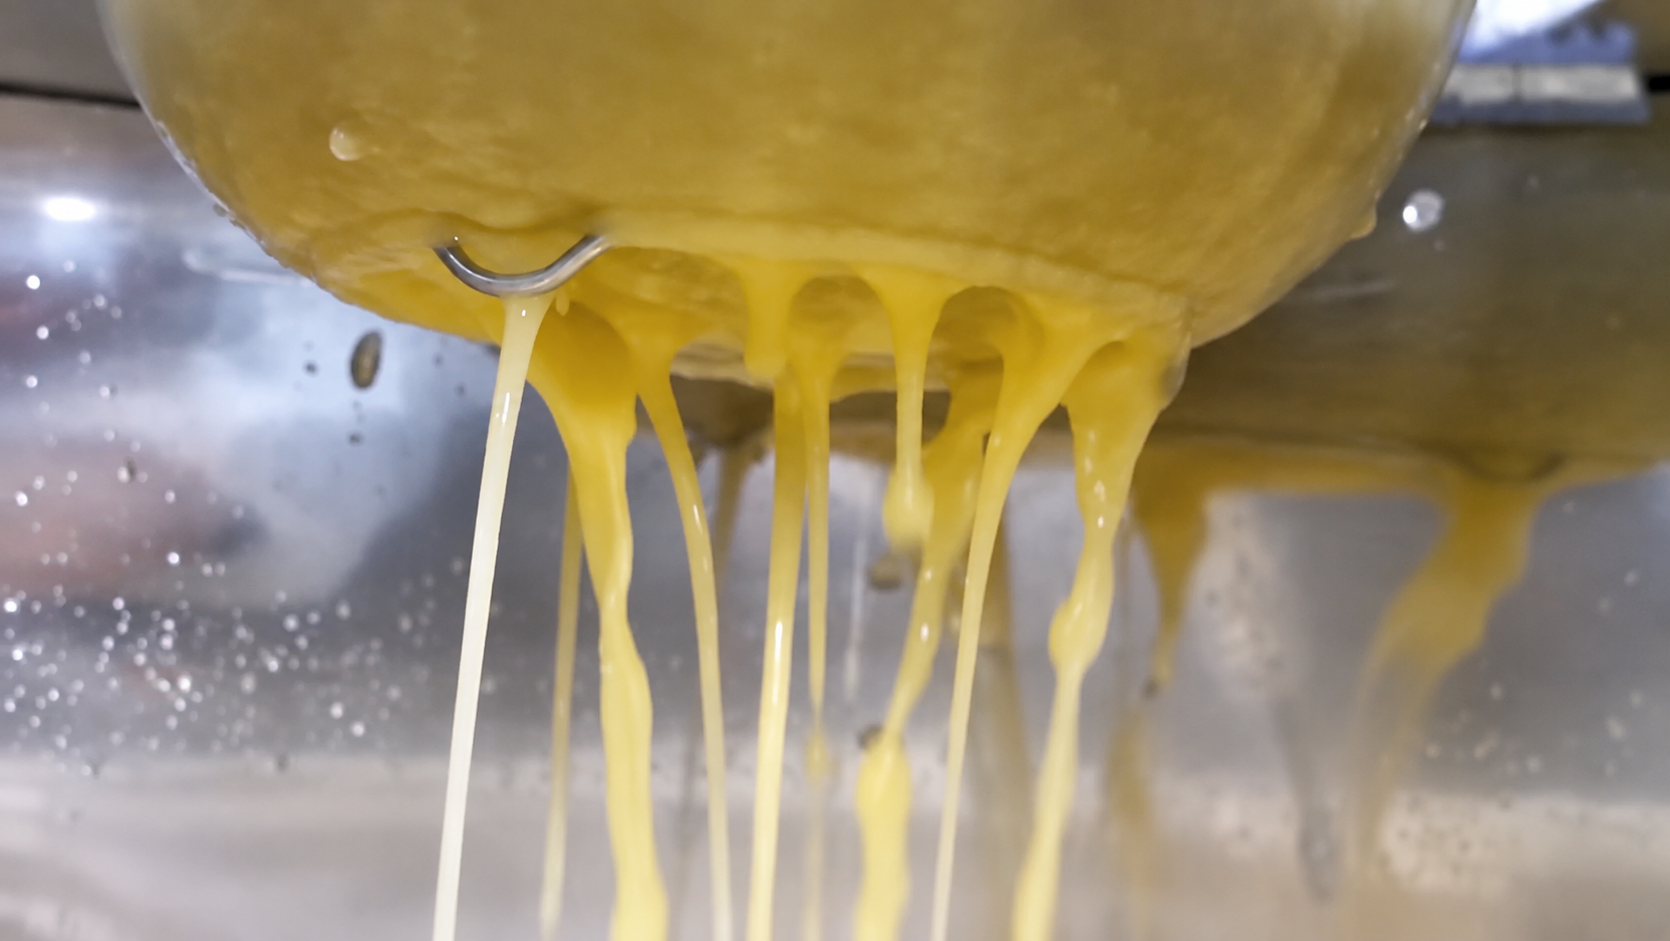
The fermentation cycle of traditional processes, which often takes dozens of days, is drastically shortened, bringing a qualitative leap in production efficiency. The maximum alcohol-to-acid conversion rate reaches 96%, greatly improving raw material utilization, with a stable ethanol-to-acid conversion rate of no less than 90%. It can continuously produce finished fruit vinegar of 3.5–9 degrees. The natural fruit aroma of fruits is retained to the maximum extent. The finished product is clear and transparent with mild and full flavor. Its bacterial indicators are 100 times better than national standards, fully complying with GB18187-2000 National Standard for Liquid Brewed Vinegar, ensuring controllable quality and safety.
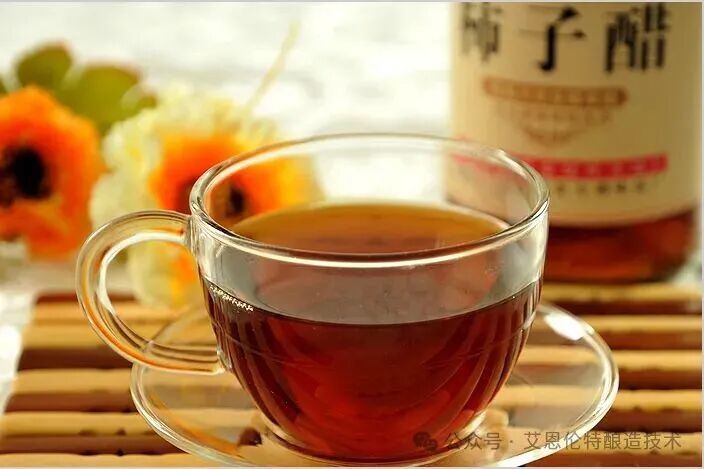
The raw vinegar produced boasts high flexibility. It can be used directly as finished fruit vinegar or formulated into fruit vinegar beverages of various flavors, greatly enriching the vinegar product portfolio to meet diversified market demands for ready-to-drink beverages and culinary vinegar. The equipment operates fully automatically with automatic feeding and automatic strain propagation. Vinegar flows out after the wine mash stays inside the equipment for 20–24 hours, minimizing quality fluctuations caused by human intervention. It suits small and medium-sized specialty fruit vinegar plants as well as large-scale production projects with an annual output of ten thousand tons.
 +86 29-87031531


 Telefon
Kommentar
(0)